Plate Merging
Key Concepts
Plate merging combines several compatible queued jobs onto a single build plate, so one printer prints them together in one run. Instead of a printer completing one small part, ejecting the plate, and starting the next, a merged plate fills the bed and prints everything at once: fuller plates, fewer plate changes, and less time spent waiting between prints. You can merge jobs yourself from the queue (manual merging), or let Printago fill the plate automatically whenever a job is matched to a printer (automatic merging, off by default). Either way, each original job keeps its own identity: the queue shows the merged plate with its member jobs nested beneath it, and every job continues to report its own status back to its order.
What Makes Jobs Mergeable
Printago only merges jobs it knows will print correctly together. All of the following must be true:
| Requirement | What it means |
|---|---|
| Compatible materials | Every job on the plate must be printable with the same filament in each slot. Jobs match when their material requirements line up on the ladder below. Single-color jobs share one filament; a plate of multi-color copies needs one loaded filament per slot, and the queue lists all of them. |
| Same printer tags | All jobs must require exactly the same set of printer tags, so the merged plate can route to the same printers any of the jobs could. |
| Same plate for multi-color | A multi-color job can be merged, but only with more copies of the same plate of the same part. Mixing different multi-color parts onto one plate isn't supported for now. Single-color jobs merge freely with each other. |
| Everything fits | All parts must physically fit on one plate together, with spacing between parts and a margin from the plate edge (both configurable, see Settings Reference). Parts are packed by their actual shape, not a square around them, so two round parts can share a plate corner-to-corner even when two squares of the same size could not. Neighboring parts sit at exactly the spacing you configured, so plates hold as many parts as the geometry truly allows. |
| Waiting in the queue | Only queued jobs that haven't been assigned to a printer can be merged. |
The Material Ladder
Jobs don't need identical material settings to share a plate. A job with a specific requirement can merge with jobs whose requirements are broader, as long as one filament satisfies everyone:
- A job that needs "Galaxy Black PLA" (a specific variant) can share a plate with a job that needs "Bambu PLA Basic" (any color of that material), a job that needs "any PLA", or a job with no material requirement at all.
- Two jobs that need different specific variants (say, Galaxy Black PLA and Jade White PLA) can't merge: no single filament satisfies both.
The merged plate takes on the strictest requirement in the group, so it only matches printers that could have printed the pickiest job on it. On a plate of multi-color copies the ladder is applied to each slot separately, and the plate lists a requirement per slot: two copies whose colors were overridden differently for the same slot won't merge, because no single loaded filament satisfies both.
What Can't Be Merged
Some jobs are excluded from merging:
- Pre-sliced files (GCODE): already sliced for a specific layout, so they can't be re-arranged.
- Parts too large for the plate: anything that doesn't fit the target plate on its own (footprint or height).
- Jobs whose size isn't known yet: Printago measures newly uploaded parts automatically within moments; until then they won't appear as merge candidates.
- Jobs whose print profiles disagree on a plate-wide setting you've configured to block merging (see How Print Settings Combine).
- A multi-color job paired with anything but its own copies: see below.
- Parts built from several model files: a ColorSCAD or CadQuery part that renders one mesh per color prints from a set of files that must be sliced together, and a merged plate carries one file per job.
- Parts with automatic merging turned off: left out of automatic merging; you can still add them by hand. See Keeping a Part off Shared Plates.
- Parts set to merge only with their own copies: automatic merging pairs them only with jobs of the same part. See Merging a Part Only with Its Own Copies.
Keeping a Part off Shared Plates
Some parts have to print by themselves: a tall piece that needs the cooling to itself, a print you watch closely, or a part that fails when another one's travel moves cross it. Open the part and, under Plate Merging, turn off Allow automatic merging with other jobs. It's on for every part unless you turn it off. With it off, Printago never puts the part's jobs on a shared plate by itself: automatic merging, the batching hold, consolidation at print time and Auto-fill remaining space all leave them out. Every other part keeps merging as usual.

You can still put one on a plate yourself. Start a merge from it with Merge..., or add it in merge mode with its Add button; hovering the button shows Automatic merging off for this part. Everything else about the plate is still checked: the job has to fit and match the plate's material, tags and print settings.
Plate Merging only affects merging. The slicer can still arrange the part on its own plate, so it is different from turning off Auto-Arrange, which keeps the part exactly where it sits in its file and also keeps it off shared plates. Several copies of the part still print as separate jobs, one plate each. A file that already holds several objects on one plate prints them together, as it always does.
To change it on many parts at once, select them on the Parts page and choose Bulk Edit. The Plate Merging column on the Parts page shows which parts merge automatically.
The setting applies to jobs already in the queue as well as new ones. A plate that was merged before you turned it off keeps the part: Unmerge that plate (see Unmerging) and the part's jobs go back to printing on their own.
Merging a Part Only with Its Own Copies
Some parts can share a plate with copies of themselves but not with other parts: a print whose settings you tuned for a full plate of it, or an order you pack and ship as a batch. Open the part and, under Plate Merging, turn on Only with copies of this part. It's available while Allow automatic merging with other jobs is on; turning that off greys it out and clears it. Automatic merging, the batching hold and Auto-fill remaining space then put the part's jobs only on plates with more jobs of the same part, and keep other parts off those plates. It works the same for single-color and multi-color parts.
You can still mix it with other parts yourself: in merge mode, its Add button shows Merges automatically only with copies of the same part on hover. It's also in Bulk Edit, and the Plate Merging column shows Same part only for parts that have it on.
Multi-Color Plates
A multi-color job merges with more copies of the same plate of the same part, and nothing else. Printing eight of a two-color keychain packs them onto as few plates as your printers' beds allow, exactly like a single-color part, and each copy keeps its own colors and painted regions.
The merged plate lists every filament it needs, numbered the way the source file numbers them: a plate that prints filaments 1 and 3 asks for filaments 1 and 3, so the slots you load line up with the colors you designed.
What isn't supported yet is mixing different multi-color parts onto one plate. Two unrelated multi-color models arranged together can spend far more time swapping filament than either would alone, so Printago leaves them as separate jobs rather than producing a plate that prints slower than the parts it replaced. A multi-color job also can't share a plate with a single-color one.
Jobs from multi-plate project files can merge. Each plate of the project queues as its own job, and merging places just that job's plate (with any skipped objects left out) alongside the other jobs on the shared plate.
Prime Towers and Dual-Nozzle Printers
A merged plate is printed exactly as it was laid out, so Printago keeps parts out of the places your printer can't print them:
- The prime tower. A plate that prints more than one filament also prints a prime tower, a small block the printer uses to clean the nozzle after each color change. Single-color plates print one too when your process profile uses smooth timelapse or wrapping detection. Printago reserves room for it on every merged plate that will print one, sized for the number of filaments, the plate's height and layer height, your filament profiles, and the slicer version the plate prints with. When a merge doesn't yet know which printer will print the plate, and a dual-nozzle printer would switch it to Bambu Studio (as happens for an OrcaSlicer store), the room fits the tower either slicer would print. Parts stay your part spacing away from the tower's brim, and never closer than 3 mm. It sets the tower's position in the plate itself, so a tower position saved in one of your process profiles doesn't move it on merged plates.
- One-nozzle strips. On dual-nozzle printers (Bambu Lab H2D, H2D Pro, H2C and X2D), each nozzle reaches less than the whole bed. A strip along one or both edges is reachable by only one nozzle: 25 mm on each side of an H2D or H2D Pro, 25 mm on the left and 5 mm on the right of an H2C, and 20.5 mm on the left of an X2D. Merged plates keep every part out of these strips, and the prime tower always sits where both nozzles reach.
The merge preview shows both: the tower as a labelled Prime tower block, and the strips as hatched One nozzle only areas. The coverage meter counts them as blocked space, and the plate thumbnails in the queue and on the job page draw them too.
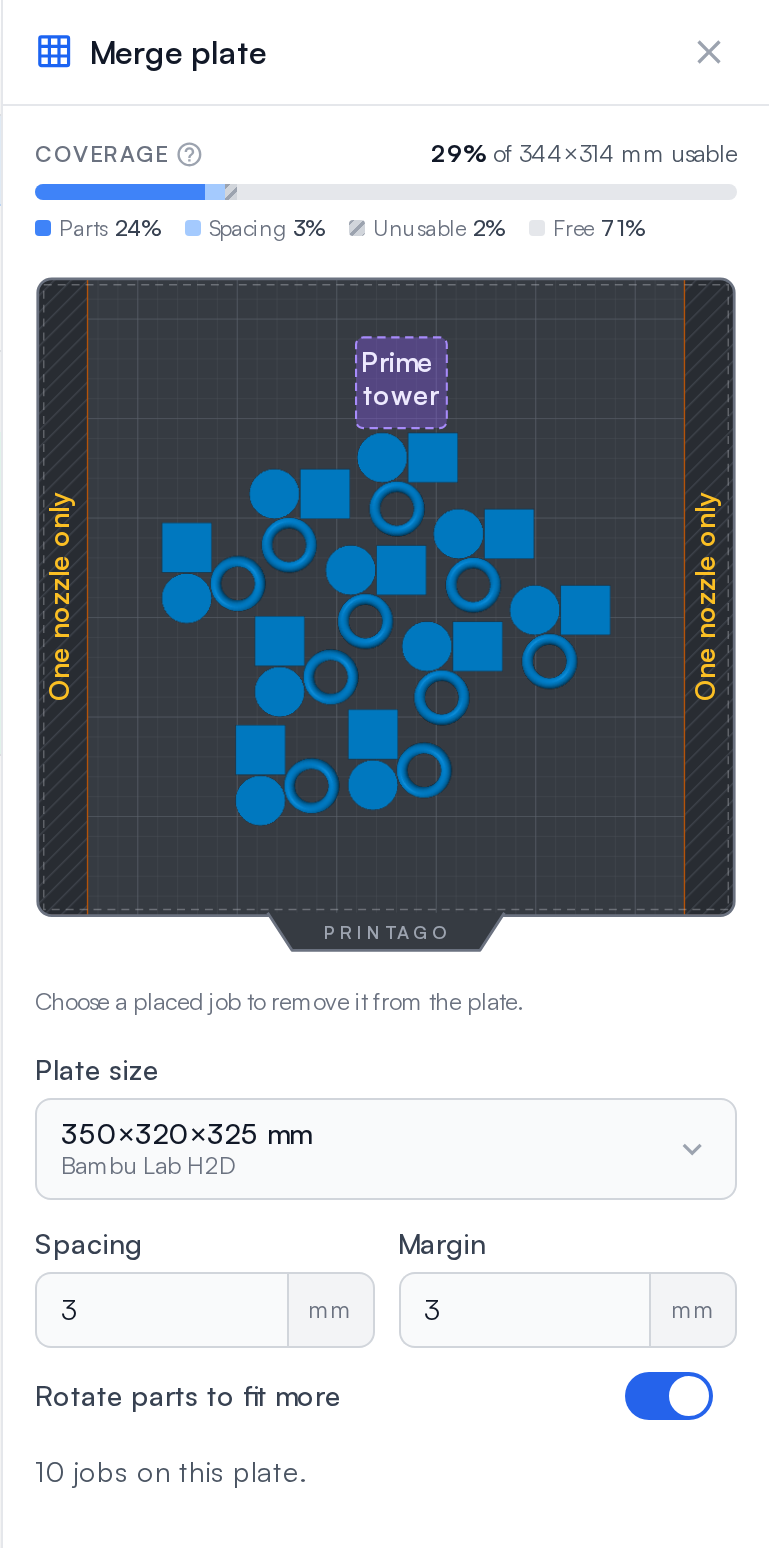
When you merge for a plate size rather than for one printer, the plate is laid out so it prints on every printer you have of that size. If you own two printers with the same bed but different keep-outs, the plate keeps clear of both, which can mean a little less room than either printer alone.
The tower's position is fixed when the plate is merged. A plate with a reserved tower therefore keeps the slicer version it was merged for, even if you change your default slicer before it prints. If you turned the prime tower off in your print settings when the plate was merged, the plate only goes to printers that also keep it off.
Part Orientation
To fit more on a plate, merging may turn a part 90° flat on the bed. It never tips a part over, so the face on the bed stays the same, but its bridges, seams, and layer lines now run the other way.
If you orient parts on purpose, for example so bridges span the short direction, turn off Rotate parts to fit more under Settings > Queue tab > Plate merging. Every part then lands on the merged plate facing exactly as it does in its own file. This applies to manual merges, automatic merges, and consolidation at print time. Plates may hold fewer parts, and a part that only fits the plate turned (a long part on a narrow bed) is reported as Too large to fit the plate and prints on its own.
The store setting is only the starting point for a manual merge: the merge panel has its own Rotate parts to fit more switch, so you can keep orientation for one plate and let another rotate freely. See Merging Jobs Manually.
How Print Settings Combine
Jobs on a merged plate can come from different print (process) profiles: one part might use an embedded profile from its 3MF file (with supports enabled, say), while another uses your store default. Merging keeps each part printing the way it was set up:
- Per-part settings follow each part. Settings the slicer can apply per object, including supports (and painted support enforcers or blockers), fuzzy skin, walls, infill, seam, brim, and even layer height, are carried onto each part individually. A part that came in with tree supports enabled keeps its tree supports; the part next to it stays support-free. Settings you set on individual objects in Bambu Studio or Orca Slicer carry over too, and every object keeps its own, so a plate whose cube has fuzzy skin and whose cylinder doesn't prints that way when merged.
- Plate-wide settings are combined by policy. Seventeen settings apply to the whole plate and can only have one value, including first layer height, skirt, prime tower, travel speed, and print sequence (see The Plate-Wide Settings for the full list). When jobs disagree on one of these, the Advanced plate optimization policies decide what happens: block the merge, take the highest or lowest value, or let the plate's profile decide.
- Jobs with no special settings never constrain a merge. A job that just uses your printer's default process profile has no opinions to reconcile; it simply adopts whatever the plate ends up with.
Which Per-Part Setting Wins
Each object on a merged plate is set up in layers. A higher layer wins, and a layer only replaces the settings it actually contains: everything it leaves out still comes from the layers below. This applies to per-object settings only; plate-wide settings are covered next.
Object and part here are the slicer's terms: a slicer part is a piece of an object, not a Printago part.
| Priority | Layer | What it contributes |
|---|---|---|
| 1 (lowest) | The printer's process profile (the printer that takes the plate) | The baseline for every setting. |
| 2 | The part's process profile | Depends on the part's Process Profile setting: Printer Default adds nothing. A named profile adds its settings, including everything it inherits from the preset it was built on, so a profile based on 0.12mm Fine that only changes wall loops still prints at 0.12 mm. Embedded 3MF Profile adds every per-object setting saved in the 3MF's project settings. The 3MF stores a complete profile, so in practice this replaces the printer's value for every per-object setting. |
| 3 | Settings on the object (right-click an object > per-object settings in Bambu Studio or Orca Slicer) | Only the settings you changed on that object, such as supports on, or fuzzy skin on one object but not its neighbor. These are kept whichever Process Profile option the part uses. |
| 4 (highest) | Settings on a part within an object (modifiers, part-level settings, painted supports and seams) | Applies only within that part's region of the object, exactly as in the source file. |
This is the same order the slicer uses when you print the job on its own, so each object on a merged plate gets the same settings it would get unmerged. What can differ is the plate-wide settings, described below.
Which Profile the Plate Uses
A merged plate is a new print in its own right, so it isn't tied to any one member job's process profile. It prints with the process profile assigned to the printer that takes the plate, with the resolved plate-wide values applied on top.
This is worth knowing for two reasons:
- "Use plate profile value" means the printer's profile, not the first job's and not your account default. If a job carried a plate-wide setting and its policy is set to Use plate profile value, that job's value is set aside and the printer's profile decides.
- The same group of jobs can print differently on different printers. If two printers have different process profiles assigned, the merged plate follows whichever one takes it. If you rely on a particular plate-wide setting, assign the same process profile across the printers that plate can route to.
Per-part settings are unaffected by all of this: supports, walls, infill, and the rest travel with each part no matter which printer takes the plate.
Compared with printing a job on its own, plate-wide settings are where a merged plate can differ:
- Embedded 3MF Profile: unmerged, the 3MF's settings replace the printer's process profile entirely. Merged, only its per-object settings carry over in full; its plate-wide settings go through the policies above, and any other whole-print setting comes from the printer's profile.
- Named profile: when checking plate-wide settings for conflicts, only the values the profile itself changes count, not the defaults it inherits. Two profiles built on different presets aren't blocked over a default neither of them chose.
The First Job on a Plate
Every merged plate has a first job, and it anchors the plate:
- Automatic merging: the first job is the one the queue just matched to a printer. Other compatible jobs are added to it in queue order, so that printer's bed sets the plate size and its loaded filament has to satisfy everything added.
- Manual merging: the first job is the one whose row menu you opened to start the merge. The order you add the rest is preserved.
- Consolidating at print time: every copy is identical, so it makes no difference which is first.
Where it matters: when a job being added conflicts with the plate on a setting whose policy is Don't merge if different, the job being added is the one left behind. The first job is never dropped from its own plate. It also determines the printer, and therefore the process profile described above.
Advanced Plate Optimization
Open Settings > Queue tab > Plate merging > Advanced plate optimization to choose a policy for each plate-wide setting:
| Policy | Behavior |
|---|---|
| Don't merge if different | Jobs whose profiles carry different values for this setting will not share a plate. Automatic merging skips them; a manual merge tells you which setting conflicted. |
| Take highest / Take lowest | The plate uses the highest or lowest value any job asks for. For on/off settings this reads as "On if any part wants it" / "Only if all parts want it". |
| Use plate profile value | Differences are ignored; the plate's own process profile decides. |
The defaults are chosen to be safe: settings that change how the whole print behaves (first layer height, spiral vase mode) block merging when they differ, speed-like settings take the safest (lowest) value, and skirt settings take the most generous value. If a value is only requested by one job and no one disagrees, it's simply adopted for the plate.
One exception to that last point: under Use plate profile value, a job's value is set aside even when every other job agrees with it, because the printer's profile always decides for that setting.
The Plate-Wide Settings
These are the settings a slicer can only apply once per plate, so they're the ones a policy has to resolve. Everything not on this list either follows each part individually or isn't affected by merging.
| Setting | Default policy | Policies you can choose |
|---|---|---|
| Print sequence (by layer / by object) | Use plate profile value | Use plate profile value, Don't merge if different |
| Spiral vase mode | Don't merge if different | Don't merge if different, Use plate profile value |
| Timelapse mode | Use plate profile value | Use plate profile value, Don't merge if different |
| First layer height | Don't merge if different | All four |
| First layer speed | Take lowest | All four |
| First layer infill speed | Take lowest | All four |
| Skirt loops | Take highest | All four |
| Skirt distance | Take highest | All four |
| Skirt height | Take highest | All four |
| Draft shield | Use plate profile value | Use plate profile value, Don't merge if different |
| Prime tower | Use plate profile value | All four |
| Prime tower width | Use plate profile value | All four |
| Travel speed | Take lowest | All four |
| Z travel speed | Take lowest | All four |
| Slicing resolution | Take lowest | All four |
| Max travel detour distance | Use plate profile value | All four |
| Ooze prevention | Use plate profile value | All four |
Some settings only offer two policies because the others make no sense for them. There's no meaningful "highest" of by layer versus by object, so print sequence can only be ignored or blocked.
Printing by object finishes each part completely before starting the next, which needs far more clearance around every part than the merge spacing setting provides. If a plate ends up printing by object, slicing can fail with a clearance error even though the parts fit on the bed.
Because the default policy is Use plate profile value, this is driven by the process profile on the printer that takes the plate, not by the jobs. If any of your printers use a by-object process profile, set Print sequence to Don't merge if different and keep those printers out of the tags a merged plate can route to.
Slicer Compatibility
A merged plate is sliced by a single slicer, so the Slicer compatibility setting (at the top of Advanced plate optimization) controls which slicers may share a plate and which one slices the result:
| Option | Behavior |
|---|---|
| Allow slicer upgrades (default) | Jobs that use the same slicer share a plate even if their versions differ, and the plate is sliced with the newest version present. For example, a job set to Orca 2.1 and a job set to Orca 2.3 print together, sliced on Orca 2.3. |
| Use account default slicer | Any jobs may share a plate regardless of their slicer, and the plate is sliced with your account's default slicer. Jobs set to different engines (say OrcaSlicer and Bambu Studio) can merge. |
| Exact slicer only | Jobs share a plate only when they use the exact same slicer and version. Orca 2.1 will not merge with Orca 2.3. |
A job's slicer comes from its part's slicer override, or your account default when the part has none. Most jobs use the account default, so this setting only matters when parts pin specific slicer versions.
Skipped Objects on Merged Plates
If you queued a job with some of its objects skipped (see Pick Objects to Print), merging respects that choice. Only the objects you kept are placed onto the merged plate; skipped objects are left out entirely, so they are never sliced or printed, and the plate's time and material estimates reflect only what you kept.
A few details worth knowing:
- The job keeps its skip selection. If you unmerge later, the job returns to the queue and still prints only the objects you kept.
- A job whose objects are all skipped has nothing to print, so it can't join a merge.
- For now, a job with skipped objects still reserves its original plate footprint on the merged plate, so a mostly-skipped job may take a little more room than the remaining objects strictly need.
Merging Jobs Manually
- On the Queued tab of the Print Queue, open a job's row menu (
⋮) and choose Merge.... If it's grayed out, hover it for the reason (see Troubleshooting below). - The queue enters merge mode: jobs that can't join the plate collapse into a single expandable row, and the remaining Compatible jobs list shows everything that can. A Merge plate panel opens with a top-down preview of the plate.
- Add jobs by clicking them (or their Add button) in the compatible list. Each added job appears on the plate preview, and the list re-filters to jobs that still fit in the remaining space. Remove a job by clicking it on the plate preview.
-
The preview draws each part's real outline: a round part shows as a circle, and parts are placed the way they will actually sit on the bed. Hover a part on the preview for a card with its size, whether its outline was measured or estimated, how it's rotated, and its distance to the nearest part. Hovering a part (on the preview or in the job list) also shows a dashed halo marking the clearance the packer keeps around it. Two halos touching means those parts are packed as tightly as your spacing setting allows.
-
The Coverage bar above the preview shows how much of the usable plate is taken. Usable means inside the plate margin and outside any keep-out area. The bar has four parts:
- Parts: the footprint of every part on the plate.
- Spacing: the clearance kept between parts. Each gap is shared by the parts on either side, so each part is charged half of the spacing setting around it. The prime tower gets the full spacing, measured from its brim.
- Unusable (hatched): gaps between parts that are too small to hold even a 1 cm part plus its spacing. Nothing else can go there.
- Free: room where at least one more small part fits, spacing included.
The headline percentage counts parts, spacing, and unusable gaps together, so a plate at 100% has no room for anything else, and it turns green once the plate is well packed. Click the ? next to Coverage for a breakdown of this plate's numbers in cm² with each part of the bar explained. Free space is not the same as a place your next part will fit: it means a 1 cm part would fit somewhere, so a large part may still be rejected while the bar shows free space.
-
While Printago works out where parts go, the preview dims and shows Arranging parts…. Big plates with many queued jobs can take a moment.
-
A part drawn with a dashed outline hasn't had its shape measured yet (for example, a part uploaded before shape measurement existed), so it reserves its full rectangular footprint. Printago measures the shape automatically the next time the part is queued, so from the following job onward it packs by its true outline; to fix it sooner, reprocess the part. Jobs that were already queued when a part's file was replaced keep their rectangular footprint: they still print the original file, so only the rectangle is known to be safe for them.
-
- Choose a plate size from the Plate size dropdown if needed. It defaults to the smallest bed size among your printers (so the plate can route to the most machines), and lists every distinct bed size in your account along with the printer models that have it. If you shrink the plate and some jobs no longer fit, they're dropped from the plate with a notice.
- Adjust spacing and rotation for this plate if needed: the Spacing and Margin fields next to the plate size override your store defaults for just this merge, handy when the parts you're combining need extra clearance (brims, elephant's foot, easy removal). The Rotate parts to fit more switch below them starts at your store setting; turn it off to keep every part on this plate facing the way it is in its file, or on to let this plate turn parts when the store normally doesn't. The preview repacks as you change them, and the committed plate always uses the same values. The next merge starts from the store settings again.
- Some printers reserve a small keep-out corner of the bed (for example, the calibration strip in the front-left corner on some Bambu Lab printers). Parts are placed around reserved areas automatically; when the selected plate has one, the preview shows it as a recessed darker patch.
- Click Merge N jobs to commit (the button enables once at least two jobs are on the plate). The queue exits merge mode and shows the new merged plate.
The preview also shows the space kept clear for a multi-color plate's prime tower and, on dual-nozzle printers, the strips only one nozzle reaches. See Prime Towers and Dual-Nozzle Printers. If the preview can't load your printers' settings, it says so: retry before merging.
Merging From a Phone
On a phone, the merge plate opens as a strip along the bottom of the screen instead of a side panel, so the queue stays in view while you pick jobs.
- The strip shows a small preview of the plate, how many jobs are on it, how full the plate is, and a Merge button you can tap at any time.
- Tap Add on a job, or anywhere on its row, to put it on the plate. Jobs already on the plate show Remove instead.
- Tap the ^ arrow at the top of the strip, tap the strip itself, or swipe it up to open the full plate. Remove a job with the × on its name, or tap its part on the plate and choose Remove. Plate size, spacing, margin, and rotation are under Plate settings, and Auto-fill and Merge N jobs stay at the bottom of the screen.
- The arrow flips to point down once the plate is open: tap it, or swipe the plate down, to go back to the queue.
Merged Plates in the Queue
- The merged plate appears as a single queued row titled Merged plate with a jobs count pill, taking the earliest member's place in line. Its thumbnail is a live top-down view of the plate layout, so merged plates are easy to spot at a glance.
- The original jobs are collapsed beneath it. Click the chevron next to the plate's title to expand them into a compact indented list, grouped like the rest of the queue: one row per part with an ×N count (shared material/tags/timing stay on the plate's row). They ride along with the plate: they can't be dragged, matched, or actioned independently while merged.
- Job and order pages for each member job continue to show that job's own status (see How Orders Stay Accurate below).
Unmerging
Changed your mind? Open the merged plate's row menu and choose Unmerge. The member jobs return to the queue as independent jobs in their original positions, and the merged plate disappears.
Unmerge is offered while the plate is still waiting in the queue, up until slicing starts. Once a plate has been sent to a printer, cancel it instead: its jobs then show as cancelled and you can retry them individually. For a plate that already failed, see A merged plate failed.
Automatic Merging
With automatic merging enabled, Printago fills plates for you. Whenever the queue matches a job to a printer, it also looks for other compatible queued jobs and adds as many as fit onto that printer's plate, in queue order. The plate size is always the assigned printer's actual bed, and the printer's loaded filament must satisfy every job added.
Enable it under Settings > Queue tab > Plate merging with the Automatically merge compatible jobs toggle.
Merge Scope
The Merge scope setting controls which jobs automatic merging may combine:
| Scope | Behavior |
|---|---|
| Same order only (default) | Only jobs from the same customer order share a plate. Jobs not linked to any order count as their own group and can merge with each other. This keeps each physical plate tied to one shipment. |
| Any compatible jobs | Any compatible jobs share a plate, regardless of which orders they belong to. Maximizes plate utilization; parts from different orders may finish together on one plate. |
Merge scope only affects automatic merging. Manual merging is never restricted by it: you can always combine any compatible jobs by hand.
Holding Jobs for Fuller Plates
By default, a job matches a printer the moment one is free, which means that on a quiet farm, ten small orders arriving a few minutes apart claim ten printers, and automatic merging never gets a chance to combine them. The batching hold fixes this: newly queued jobs wait briefly for companions, so those ten orders can come off one printer as one full plate. Fewer print starts also means fewer bed heat-ups, purge sequences, and plate changes, so less energy and less operator time for the same parts.
Set Hold time (minutes) to how long a new job may wait (0 disables holding, the default). While held, the job shows a Waiting to batch tag in the queue with the time remaining. A held job never waits longer than the hold time, and it's released early the moment waiting stops paying off:
- The plate is full enough. Once the jobs that would merge together fill the Release when plate is this full (%) threshold of the plate, they print immediately. Ten quick orders may release after two minutes, not fifteen. Fullness is measured exactly like the Coverage bar in the merge preview: parts, the spacing around them, and gaps too small for anything else all count, so a plate the packer can't fit one more part onto reads as full even when the parts themselves cover less of it.
- The plate hits the max parts limit.
- The job can't merge anyway (for example a pre-sliced or oversized part): it prints right away, since holding it can't help.
A few things to know:
- Each job's hold is anchored to when it was queued. A steady trickle of new orders can never postpone an earlier job past its own hold time.
- Held jobs can still join another job's plate: if an older job releases and merges, waiting jobs are swept onto its plate immediately.
- Match queue now (on the queue page) bypasses all holds, and Send to... on a job prints that job immediately. Use either as the rush-order escape hatch.
- The hold only batches jobs that merge scope allows together. Under the default Same order only scope, jobs from different orders won't combine, so cross-order batching (the ten-orders example above) needs Any compatible jobs.
- The trade-off: fuller plates concentrate risk. One failed first layer affects everything on the plate, and every job on it finishes when the whole plate does.
How Orders Stay Accurate
Merging never blurs order tracking. Each original job stays linked to its own order and mirrors the plate's progress as its own status: when the plate starts printing, each member job shows as printing; when it completes, each shows as completed. Order pages read status from their own jobs, so they stay correct even when the physical print is a shared plate.
Consolidating at Print Time
When you print several copies of a part (say a run of 100), you usually don't want 100 separate jobs marching through the queue one plate-swap at a time. Consolidation packs those copies onto as few full plates as possible right when you print, so a part that fits 20 to a plate becomes 5 merged plates instead of 100 jobs.
Turn it on with the Consolidate onto plates toggle in the print dialog. It's available when printing a part, a SKU, or an order, right below the priority and position controls. When enabled you can pick the plate size and adjust spacing and margin for this print, exactly like a manual merge; they default to the smallest bed among your printers and your store's spacing settings.
How the copies are packed:
- Copies are packed onto full plates in order; each full plate becomes one merged plate in the queue (with its copies collapsed beneath it, and the top-down plate thumbnail).
- A leftover copy that can't fill a shared plate, or any copy that can't be merged (pre-sliced or too large for the chosen plate), simply prints as its own normal job. Copies of a multi-color part consolidate like any other, since every copy is the same plate.
- Consolidated plates are ordinary merged plates: each copy still tracks back to its own order, and you can un-merge a plate at any time before it slices to split it back into individual copies.
A consolidated plate is built for the plate size you chose, so it only prints on a printer whose bed is at least that large. If nothing in your fleet has a big enough bed, the plate waits. Pick a smaller plate size, or un-merge it into copies that any printer can take.
Consolidation and automatic merging work together: consolidation packs the copies of one print at creation, and automatic merging can still combine leftover single copies with other compatible jobs later.
Settings Reference
All plate merging settings live under Settings > Queue tab > Plate merging.
| Setting | Default | Description |
|---|---|---|
| Automatically merge compatible jobs | Off | When a job is matched to a printer, also fill that printer's plate with other compatible queued jobs. |
| Merge scope | Same order only | Which jobs automatic merging may combine: Same order only or Any compatible jobs. |
| Hold time (minutes) | 0 (off) | How long a newly queued job may wait for compatible companions before printing, so jobs arriving close together share one plate instead of each claiming a printer. See Holding Jobs for Fuller Plates. |
| Release when plate is this full (%) | 80 | Ends a hold early: once the batch fills this much of the plate, it prints immediately instead of waiting out the hold time. Measured like the merge preview's Coverage bar (parts, spacing, and unusable gaps), so 100 means nothing else fits. |
| Part spacing (mm) | 3 | Minimum clearance between parts placed on a merged plate, and between parts and the prime tower's brim. Manual merges can override this per plate. |
| Plate edge margin (mm) | 3 | Keep-out margin from the edge of the plate. Manual merges can override this per plate. |
| Rotate parts to fit more | On | Lets merged plates turn a part 90° when that fits more parts. Turn it off to keep every part facing the way it is in its file. Manual merges can override this per plate. See Part Orientation. |
| Max parts per plate | 50 | Upper bound on how many parts one merged plate can hold. |
| Advanced plate optimization | Safe defaults | Per-setting policies for combining plate-wide slicer settings when jobs with different print profiles merge. See How Print Settings Combine. |
| Slicer compatibility | Allow slicer upgrades | Which slicers may share a plate, and which one slices the result. See Slicer Compatibility. |
Troubleshooting
Why does a job say "Waiting to batch"?
The batching hold is on, and the job is waiting (up to the configured hold time) for compatible jobs to share a plate with. It prints sooner if enough jobs arrive to fill the plate. To print it right now, use Send to... on the job, or click Match queue now to flush every hold. If jobs from different orders aren't combining during the hold, check that Merge scope is set to Any compatible jobs.
Why is Merge disabled?
Hover the disabled Merge... entry for the specific reason. Common ones:
| Reason | What to do |
|---|---|
| No compatible jobs | Nothing else in the queue matches this job's material, tags, and plate. Queue more of the same work, or loosen material requirements (e.g. "any PLA" instead of a specific color) on parts where color doesn't matter. |
| Dimensions haven't been computed yet | Newly uploaded parts are measured automatically within moments. Wait a little and try again. |
| Pre-sliced GCODE files can't be re-arranged | Pre-sliced jobs can't be merged. Queue the original model file instead if you want it merged. |
| Multi-color plates can only be merged with copies of themselves | A multi-color plate merges with more copies of the same plate, and nothing else. Queue more copies of that part, or merge the single-color jobs separately. |
| Parts built from multiple model files can't be merged | The part renders a separate model file per color (ColorSCAD, CadQuery). Those files have to be sliced together, so the job prints on its own plate. |
| Too large to fit the plate | The part doesn't fit the target plate on its own, so it can't share one. With Rotate parts to fit more off, a part that would fit only turned 90° also lands here. |
| Print settings conflict | The selected jobs' print profiles disagree on a plate-wide setting whose policy is Don't merge if different. Change the policy under Advanced plate optimization, or merge the conflicting jobs onto separate plates. |
Why won't a merged plate go to a free printer?
A merged plate is laid out for a specific plate size, so it only prints on a printer whose bed is at least that large on every side. Parts are placed at fixed positions, so the printer must also be able to print where they sit. Click Printer Matching on the plate in the queue and pick the printer: its Fits the bed check shows why it can't take the plate.
- Larger than this printer's bed: the check shows the plate size next to the printer's bed size. Wait for a printer with a bigger bed, or Unmerge the plate so its jobs can be arranged for that printer.
- Parts in an area of this printer's bed it can't print on: a part sits on a keep-out corner of this printer's bed. This happens when a plate was merged before the printer joined your fleet. Another printer of that size can still take it, or Unmerge the plate and merge it again so it's laid out for this printer too.
- Parts in a strip only one of this printer's nozzles reaches: the same, on a dual-nozzle printer whose one-nozzle strip has a part in it.
- Prime tower spot: the check says what's wrong with it. The plate has no spot for the tower this printer prints, the spot is in an area the printer can't print on or where only one of its nozzles reaches, or it's too small for this printer's tower. Unmerge and merge again.
- Couldn't load this printer's profiles: Printago couldn't read the printer's machine or process profile to check the plate. Open the printer's settings, check both profiles are assigned and still exist, and the queue checks again on its next run.
A merged plate failed
If a merged plate errors, the whole plate fails together, and each member job shows as errored on its order. Nothing un-merges automatically. You have two options:
- Retry the plate: retries the entire merged plate as one print. Best when the failure was situational, like a filament runout or a knocked-loose part.
- Split it back up and retry the jobs individually: best when the plate itself is the problem, for example when it won't slice.
Unmerge is only offered while a plate is still waiting in the queue, so a failed plate needs an extra step: click Retry first, which returns the plate to the queue, then Unmerge it before the queue matches it to a printer again. Pausing automatic matching first makes this reliable. The member jobs then return to the queue as independent jobs and you can retry only the ones you need.
If a merged plate fails to slice, splitting it up is almost always the right move: the same group of jobs will fail the same way on a retry.
Jobs vanish from the compatible list
While you're building a plate in merge mode, the queue keeps running. If a printer picks up one of the compatible jobs (or another user merges it), it leaves the list, since it's no longer available. If you want the queue to hold still while you arrange a plate, pause Automatic Queue Matching first (see Pausing Automatic Matching).
Related Topics
- Print Queue: how jobs are queued, matched, and managed
- Pick Objects to Print: skipping objects on a plate before printing
- Materials: material types, materials, and variants
- Printer Tags: routing jobs to groups of printers
Questions about plate merging? Join our Discord community for the latest tips and support!